Piston / plunger
The replacement photo shows a head and long stem. The bench shape follows that form; head diameter, stem size, length, surface condition and seat are unverified.
The factory 1500 plate lists a piston, spring, copper sealing washer and long hex plug. This block-mounted assembly is separate from the oil pump and the spin-on filter. Its parts have not been identified or measured on this car.
The main engine CAD does not yet contain this assembly. The separate four-part STEP uses an exploded bench layout with no engine coordinates. Two dimensions have documentary anchors below; every other size and profile is an estimate. The drawing and STEP explain component relationships, not tool access, installed spring compression or a removal path.
The manual also prints 1.53 inches. The STEP follows its metric value; the figures are rounded equivalents. This does not establish installed length, preload, rate or relief pressure on this car.
The replacement listing identifies a copper crush washer. Its outside diameter, thickness and the fitted washer remain unmeasured.
Four separated parts, in millimeters. The gaps are display spacing; the parts stay in this bench layout while you inspect them.
Loading the four-part reference…
Choose a part to see its evidence basis.
Drag or use arrow keys on the canvas to rotate. Pinch, scroll or use the zoom slider to magnify. Tap a shape or use the part buttons to select it. No installed pose, compression or service movement is shown.The illustrations are unscaled recognition diagrams. The factory plate MB0699, PDF page 61, printed 107-B85/B86 lists one of each at items 12–15.
The replacement photo shows a head and long stem. The bench shape follows that form; head diameter, stem size, length, surface condition and seat are unverified.
The bench spring has the UK manual's 38.8 mm free envelope. Coil count, wire diameter, winding direction, end treatment and spring rate are estimated or unmodeled. A matching free length alone cannot identify or calibrate a spring.
The factory plate specifies one copper washer. The workshop page calls for renewal on refit. The bench ring's 14 mm opening is a replacement comparison; its outer size, section and compression are estimates.
The replacement photo shows a long hex body, threaded shank and opening. The STEP uses an unthreaded shank and a blind display bore. Hex size, thread, engagement, internal depth and tightening specification need fitted evidence.
IMG_6966, IMG_6967–6970 and IMG_6897 show the fitted filter/distributor side, but no relief body can be confidently identified in the reviewed views. There is no verified photo hotspot or engine placement for this assembly. These two views help plan the missing capture; they do not identify a hex head as the relief plug.
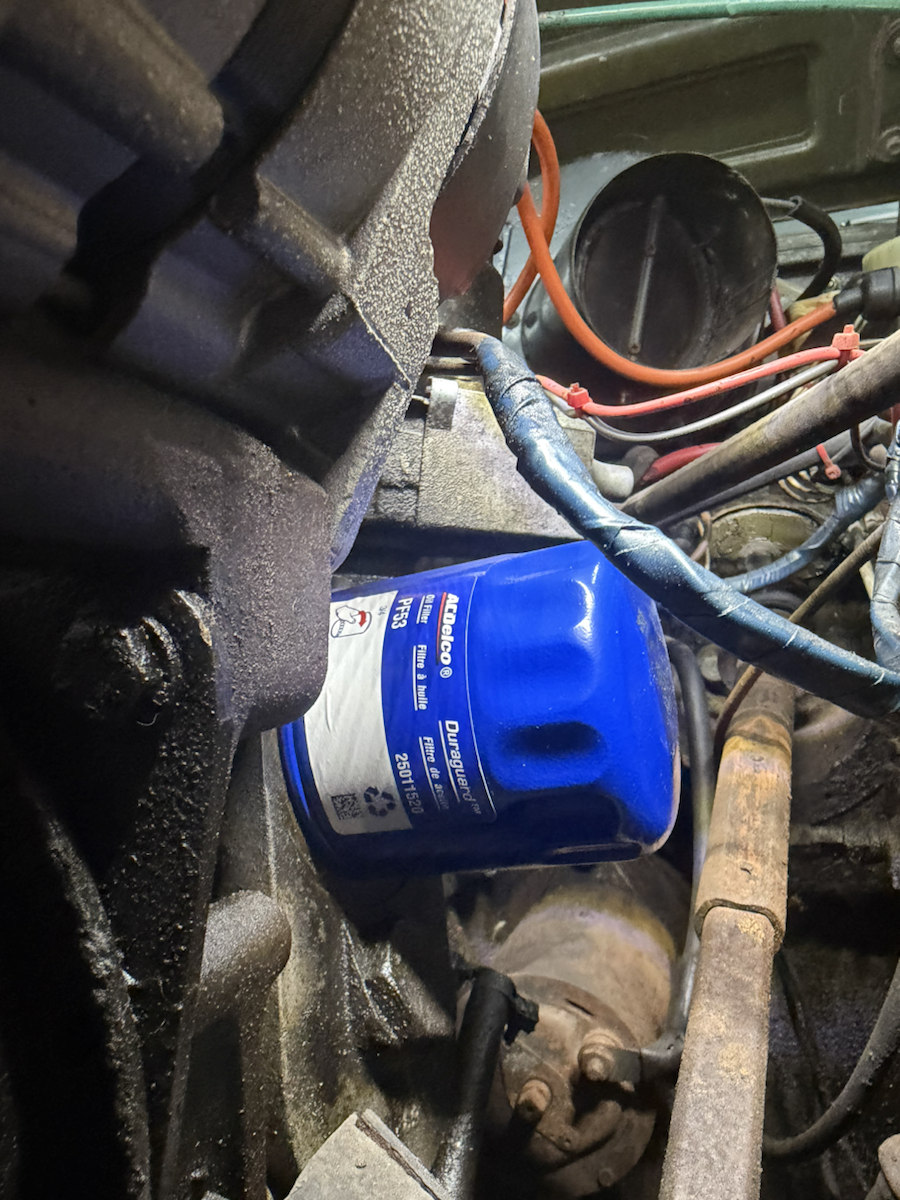
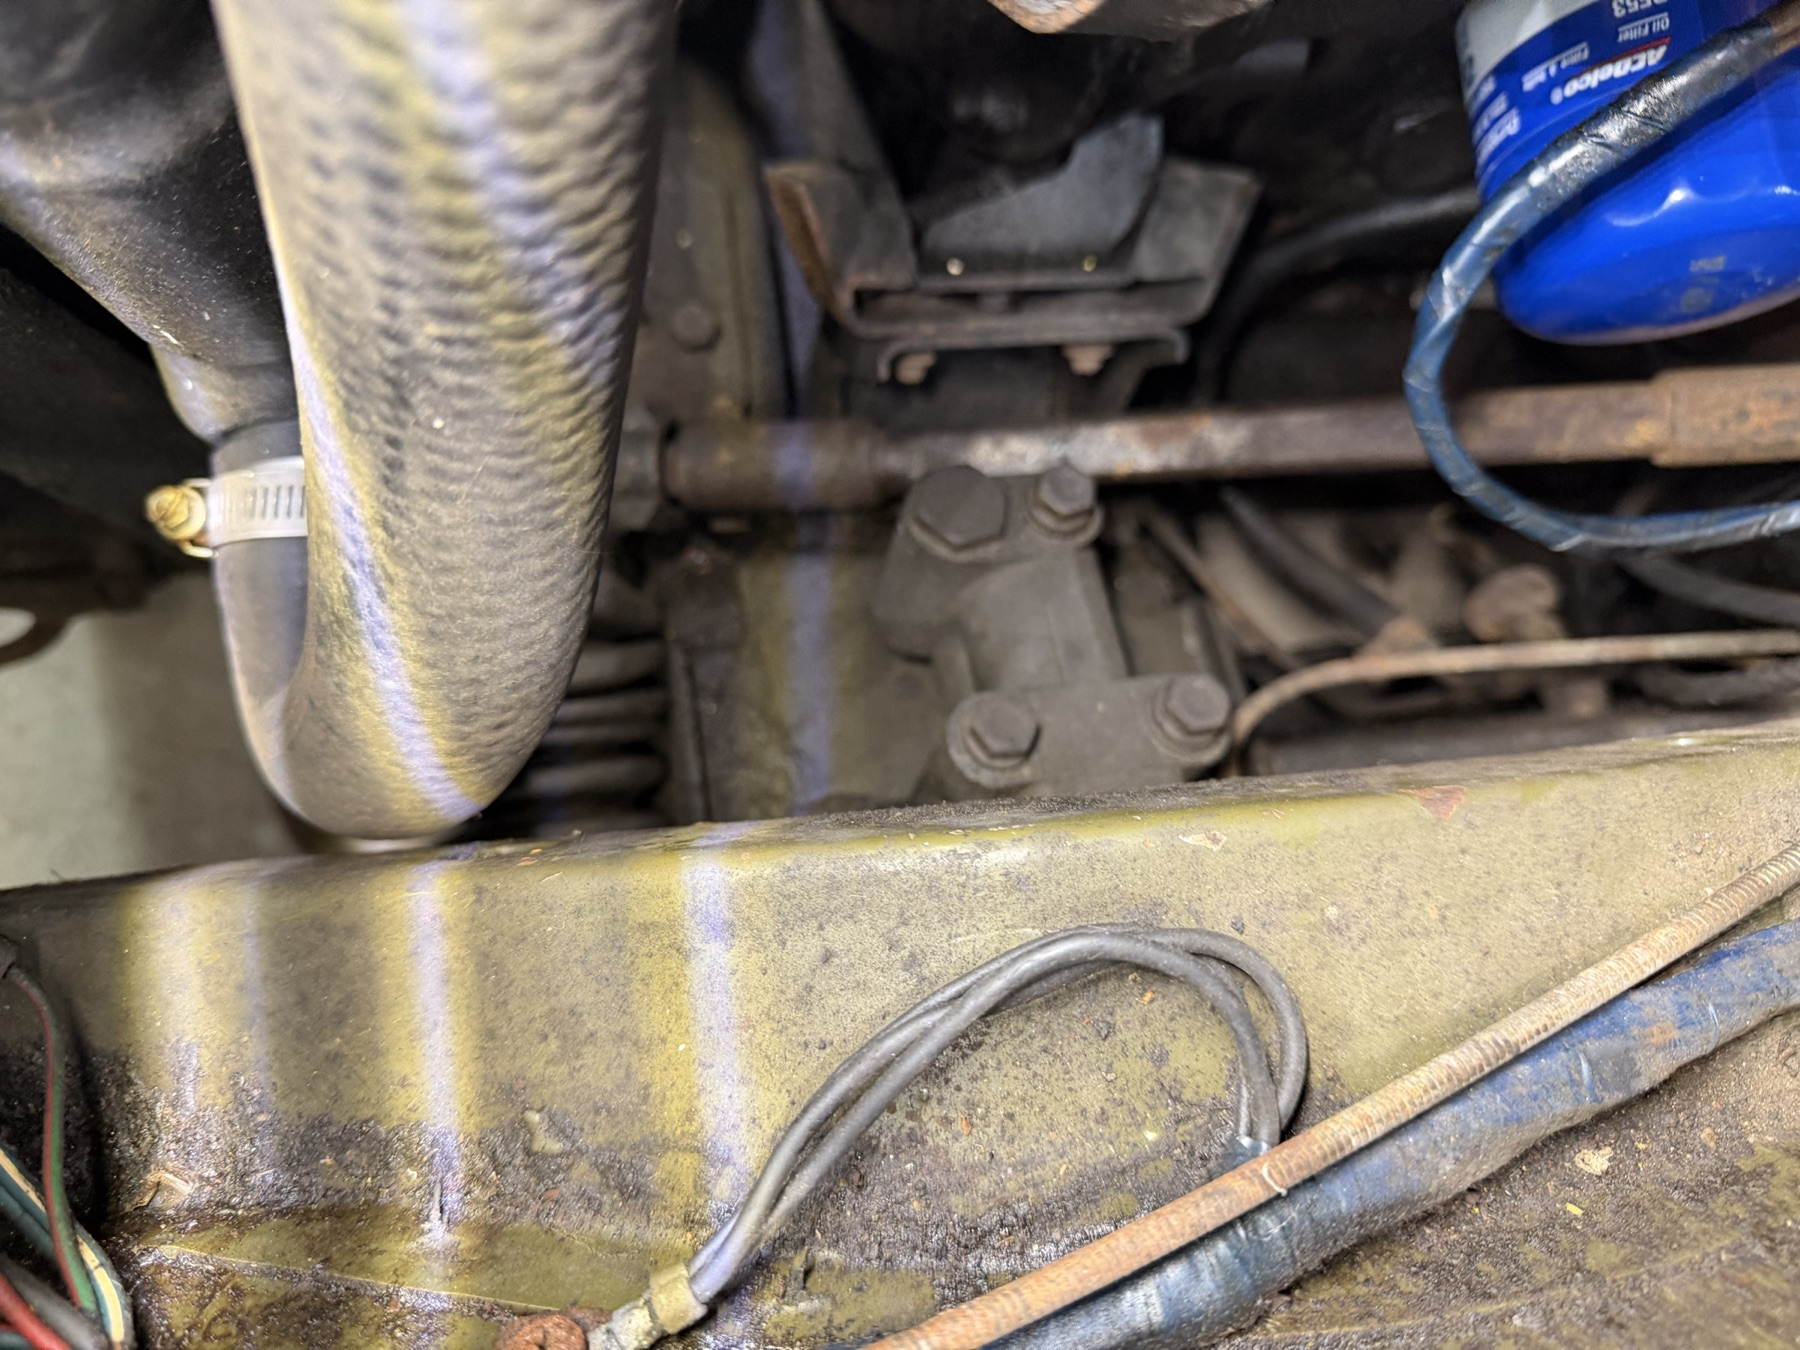
For a useful fitted record, pair a whole-side view with a close side view that shows the positively identified body from block joint to outer end. Put a scale in the same plane and record the view direction and named nearby datums. A head-only close-up cannot establish the hidden axis, projection or available tool space.
Operation 12.60.56, PDF page 11, printed page 84 is headed Engine—U.K. Specification. Its component sequence is: remove the body from the block, discard the removed washer, withdraw the plunger, then remove the spring. Refit reverses that sequence with a new washer; the manual calls for a replacement spring when its free length does not agree with the data.
That source does not establish the fitted North American assembly, socket clearance, thread specification, tightening torque or pressure calibration here. Keep it as a reference until the actual parts and applicable instructions are confirmed. The exploded bench gaps are display spacing, not withdrawal distances.