See what the clutch
joins together.
The whole-car reference now separates a static flywheel, driven plate, unloaded facings, pressure plate, diaphragm and hollow cover. The retained release mechanism remains behind it with an unresolved drawing gap. Select the components to inspect the clamping stack and its surrounding references.
Inspect the whole-car clutch stack ↗The Midget 1500 engine plate lists four flywheel bolts and one locating dowel; its clutch plate lists the driven disc, cover, release bearing and six cover setscrews. A 1975–79 replacement disc listing gives the 7¼-inch outside diameter and 20 splines; a ring-gear listing gives 117 teeth. The car's installed disc, gearbox and flywheel have not been inspected. Rimmer's Spitfire 1500 flywheel listing distinguishes early US ⅜-inch and later 7⁄16-inch crank-bolt versions; the Midget's fitted bolt size must be checked directly. Flywheel diameter, clutch cover profile, axial stations, bolt circles and release-bearing clearances in CAD are estimates. This is not a removal path, torque chart or resurfacing drawing.
A connected clamping-stack reference
The previous flywheel had an estimated 88 mm central recess radius. Most of the reference friction annulus therefore faced a recess, and the flat cover cue contained no separate pressure-plate role. The current whole-car overlay retains the flywheel outer envelope, crank/bolt/dowel datums and engine placement, reduces that unmeasured recess to 50 mm, and adds six plain cover-fixing passages. These are construction corrections to the drawing, not machining dimensions or an inspection of the fitted flywheel.
Two unloaded facing annuli now share explicit planes with the flywheel and separate pressure plate. A larger steel core, retained visual hub/damper roles and added carrier web replace disconnected source regions. A thin domed shell, conical diaphragm/support and three illustrative drive straps explain the cover assembly. Six smooth screw/washer roles follow the retained drawing axes. The old ring gear, four crank fixings, three locating dowels and pilot bush keep their original geometry and pose.
Factory and catalog evidence
Factory 1500 plate, PDF p. 79, distinguishes GCC196 cover, GCP230 driven plate, GRB207 release bearing and six 146176 screw/LWN305 washer roles. The general specification supplies nominal 7¼-inch diameter. The replacement disc listing gives 20 splines, and the MGOC list attributes 1/4 UNF to 146176. None identifies the installed clutch.
Construction estimates
Recess size, friction inner diameter/thickness, core/hub details, cover depth/gauge/windows, pressure plate, spring fingers/support, strap count/shape, axes, screw length/head and plain bores remain estimates. The smooth damper-role cylinders and unioned carrier show a static assembly envelope; they are not a model of torsional springs or welded ownership. The visual hub slots do not define a mating spline profile.
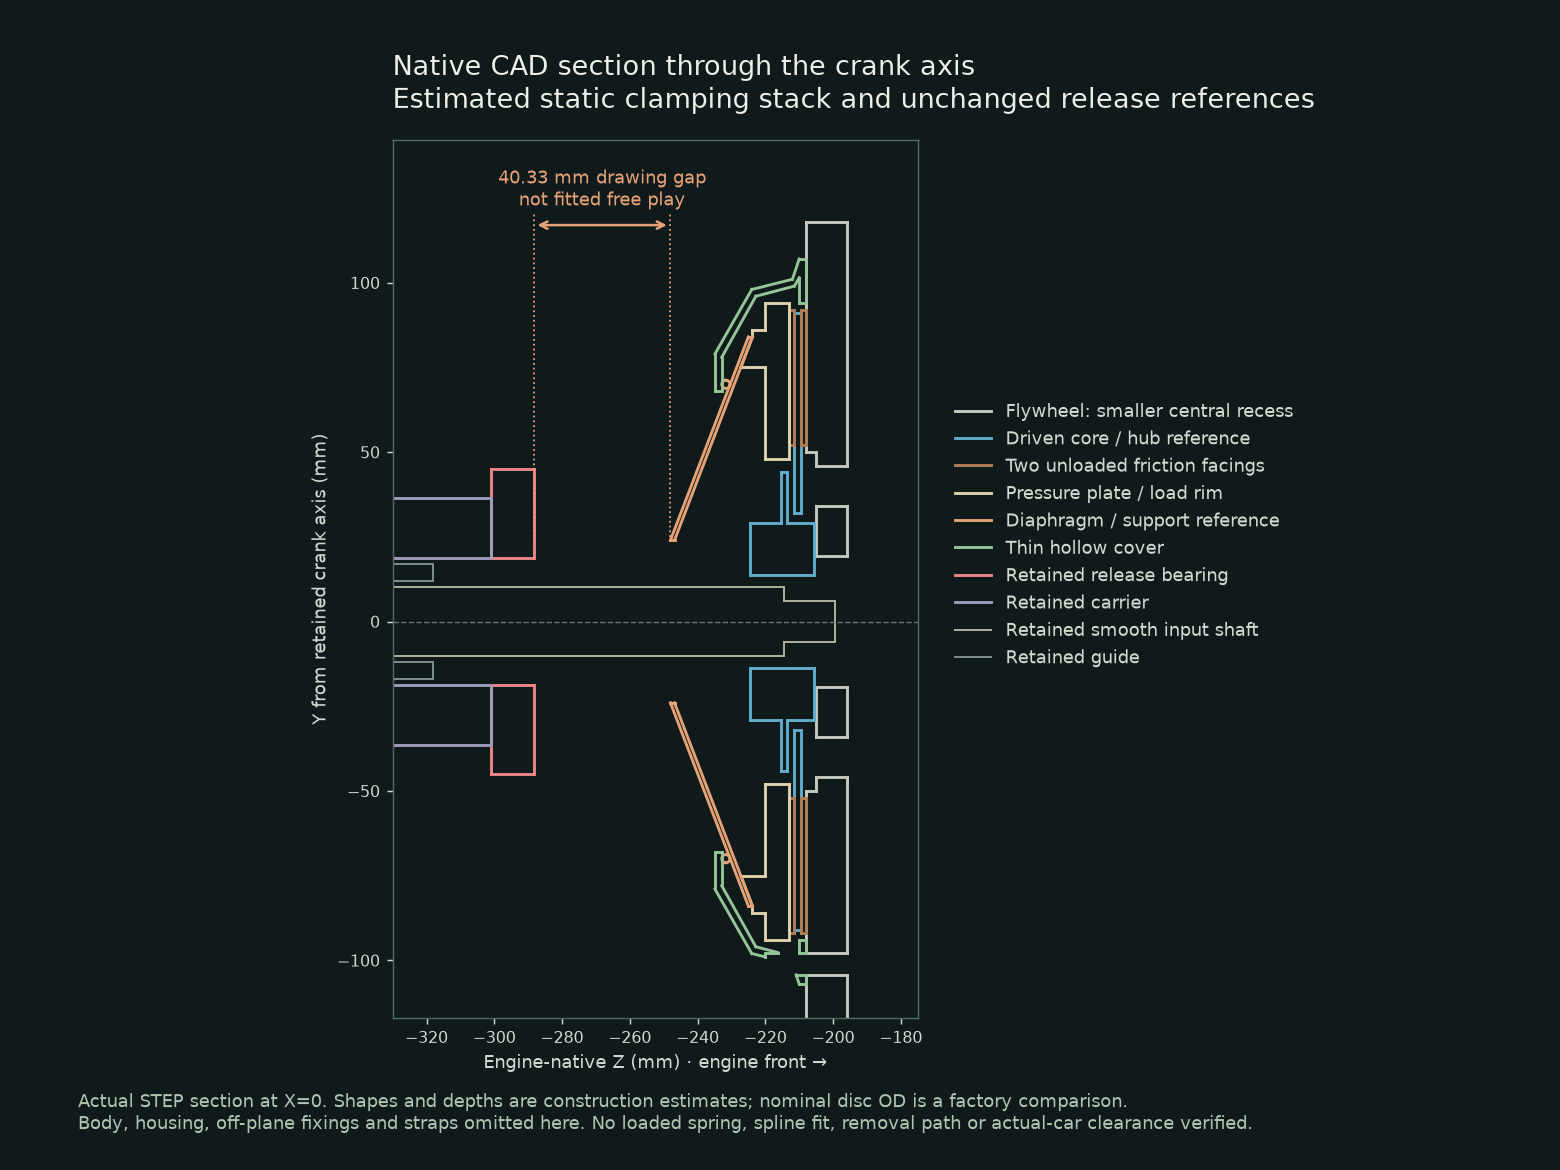
Keep the unresolved interfaces visible
The new diaphragm inner reference plane remains 40.333 mm ahead of the unchanged release-bearing front. The earlier 58.333 mm value compared that bearing with the old flat cover envelope. Neither value is fitted free play or release stroke, and neither justifies extending the carrier. Engine/gearbox placement, housing/plate faces, fork, slave, carrier and bearing remain in their prior frames. No source-pack/housing intersections occur in the selected static comparison; that does not verify loaded or removal clearance.
The retained smooth input shaft and circular/scalloped hub bore do not form verified mating splines. The input/pilot-bush source intervals overlap by only about 2.067 mm; that is a drawing calculation under estimated transforms, not an approved engagement length or fitted bearing clearance. Actual hub orientation, cover contact depth, carrier/bearing identity and installed interface dimensions remain unresolved in the evidence used here.
The study omits body, clutch housing and most gearbox geometry so the stack and remaining gap can be seen. Use the whole-car view to restore surroundings. Separation offsets do not establish support, release order, tool access, diaphragm unloading, clutch alignment, tightening or a verified withdrawal path. Internal cover roles are shown for anatomy; their display does not establish a serviceable cover repair or a dismantling sequence. Factory parts diagrams supply roles and quantities, not those operations.
The five superseded engine meshes remain visible if the new pack cannot load in the whole-car view. On successful loading, four retained engine source groups become separately selectable without changing their pose. The detailed engine-only study preserves its earlier clutch cover/disc geometry, while sharing the revised catalog ring and flywheel support; it is a separate source comparison.
Validation covers eight positive native groups, open cover/flywheel fixing bores, supporting material across the constructed contact annuli, selected internal nonintersections, preserved crank/dowel/pilot geometry and mesh/STEP fidelity. It does not establish clamp load, spring travel, friction, spline engagement or actual-car fit. The rear-drive scale correction below revises the ring, support radius, starter pose and surrounding plate/housing; bearing and shaft registration gaps remain explicit.
A larger ring gear changes the surrounding assembly
The previous ring gear was about 252 mm across. The factory 1500 parts plate identifies 201350; the County RG291X replacement listing gives 117 teeth,11.849 in outside diameter,10.629 in bore and0.500 in width. The revised reference uses 300.9646 mm OD,269.9766 mm bore and12.7 mm width. These are offered-part dimensions, not measurements of this car.
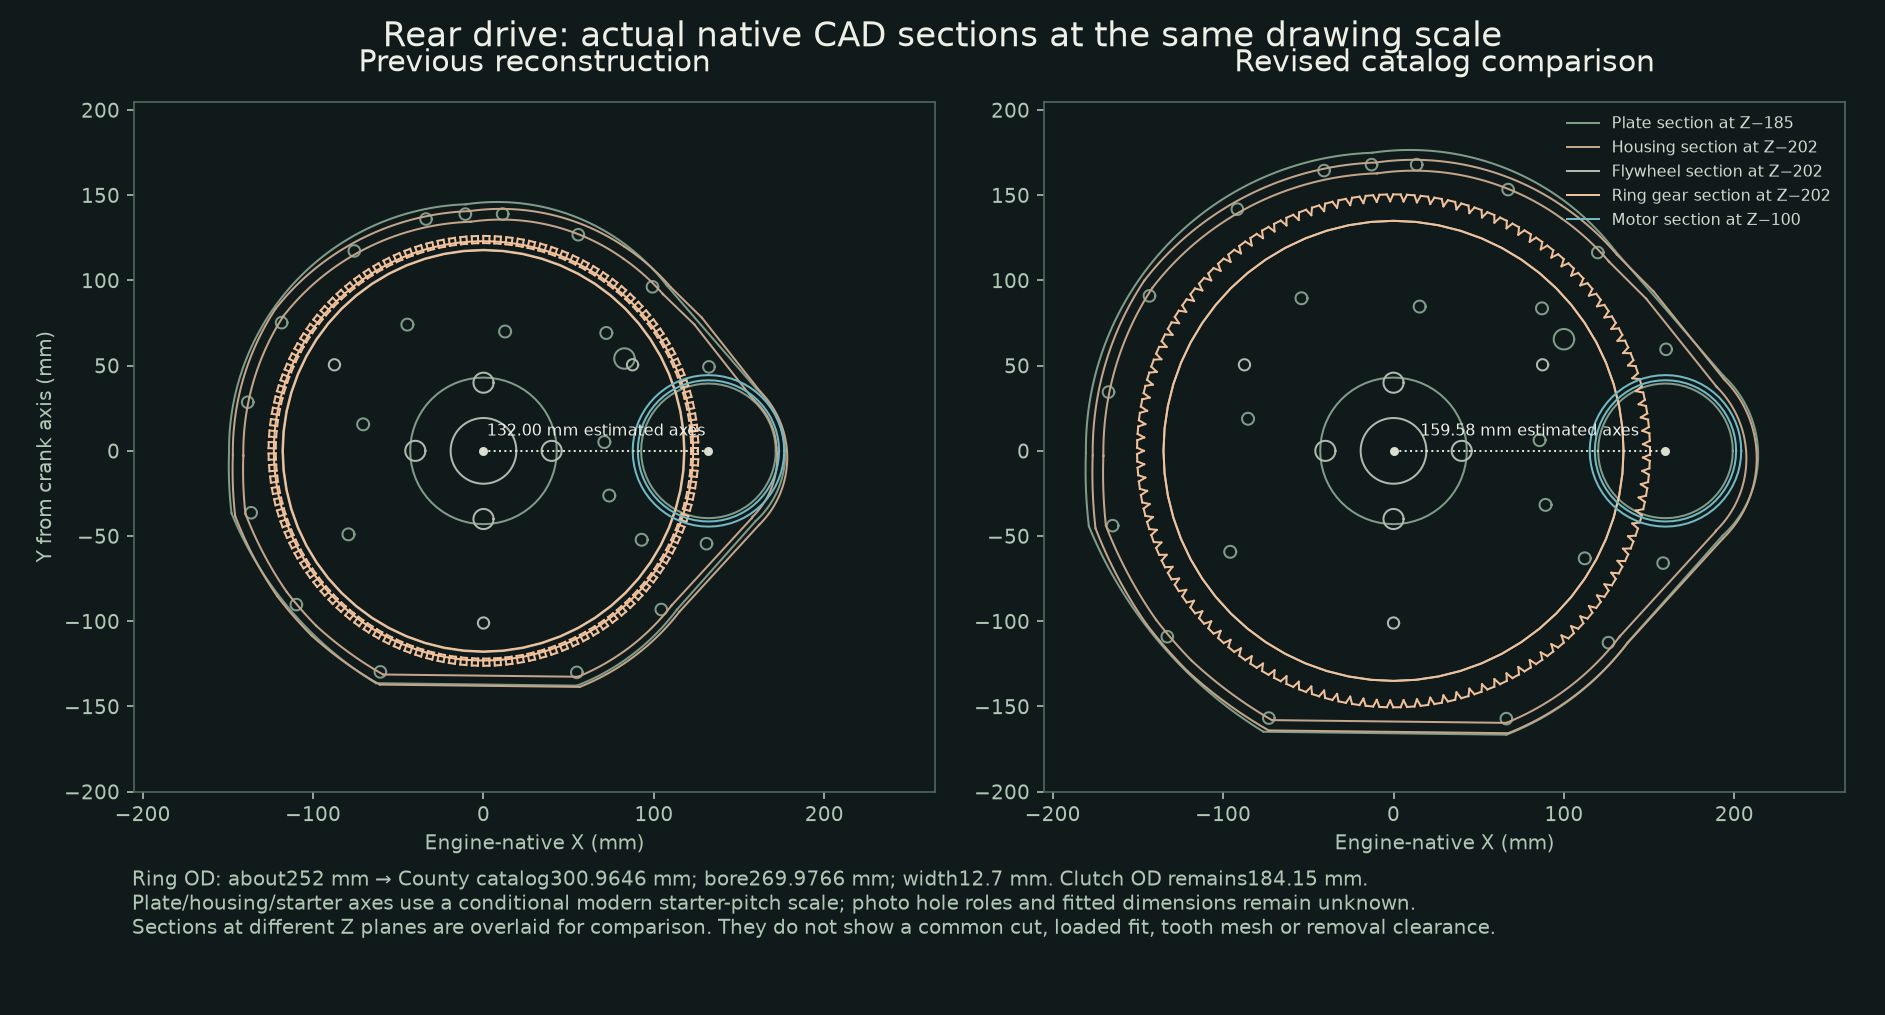
CEP separately cross-references 201350 with 117 teeth,11.847 in OD and1/2 in width. Its 10.645 in turn diameter is a flywheel machining reference, not a ring bore. It differs from the County bore by 0.4064 mm. The model does not turn those separate catalog products into a shrink-fit allowance or machining instruction. Tooth flanks and root depth remain illustrative; no DP, bevel direction, involute or working engagement is established.
The flywheel support radius follows the County bore for a zero-interference illustration, while the nominal 184.15 mm clutch and crank/clutch axial planes stay fixed. Plate and housing outlines now share a conditional 125.45 mm compatible modern-starter pitch scale applied to two candidate holes in the replacement-plate photograph. This gives a 159.5849 mm crank/starter axis separation. The hole roles, photographic projection, original M35J pitch and fitted scale remain unverified. All 24 photographed holes remain unassigned.
The 20 starter groups share an estimated 11.5 mm forward shift: the drive-end flange now meets the estimated plate front rather than straddling it. Two plain fixing envelopes cross the estimated plate/flange thickness; their length, head orientation and fitted washer/nut retention remain unknown. Selected native checks find no intersection of the revised ring/flywheel with the housing or of the yoke/drive-end flange with the plate/housing. This does not validate the whole car, drilling alignment, gear engagement or starter withdrawal.
Inspect revised ring gear in the whole car ↗ Select the starter drive end ↗The 40.3333 mm release-bearing/diaphragm drawing gap remains open. The next substantial priority is to reconcile that axial stack from documentary evidence without extending a shaft or carrier merely to close the picture. The native validation record states the checks and remaining source intersections.
Earlier engine-only clutch reference
Flywheel and ring gear
The crank turns the flywheel through four bolts and a locating dowel. The model also shows a separate pilot bush, scaled to a matching-family 1-inch × ½-inch ID × ¾-inch OD replacement listing. The ring gear is a separate 117-tooth study outside it; its tooth profile is provisional.
Select ring gear ↗ · Select pilot bush ↗Driven plate
The modeled outside diameter uses the listed 184.15 mm comparison part. The separate segmented facings and 20-slot hub show the visible structure in a matching-family kit photograph; they are not spline or friction-thickness gauges.
Select driven plate ↗Cover and six screws
The cover clamps the driven plate to the flywheel. Six screws and three cover locating dowels are shown at approximate stations. The spring mechanism and exact bolt positions need the fitted cover.
Select cover ↗Release bearing
The separate bearing sits behind the cover in the gearbox-side mechanism. This earlier engine-only envelope omits the carrier/fork. The whole-car inspection view includes separate carrier/fork references; fitted travel remains unresolved.
Select bearing ↗Planning a clutch project
- Identify the engine and gearbox, and read the installed clutch or service history before ordering a kit. The modeled 20-spline disc is a comparison part.
- Plan access using the workshop procedure for the actual car. The whole-car reference supplies gearbox, housing, exhaust, mount and body obstacles in estimated frames. Neither view establishes fitted access or an extraction route.
- Reconcile the supplied photographs, measurements and service notes for cover marks, fixing positions, release mechanism, disc orientation and spline count. Keep unobserved identities and dimensions unknown; the current model does not supply them.
- Inspect the flywheel friction surface, ring-gear teeth, pilot bush and crank-to-flywheel fasteners as separate items. Measure worn parts using the applicable workshop specifications and identify any previous machining.
- Use the correct alignment tool, fitted parts and factory tightening procedure for reassembly. The explode slider shows relationships only; its offsets are not safe removal travel.